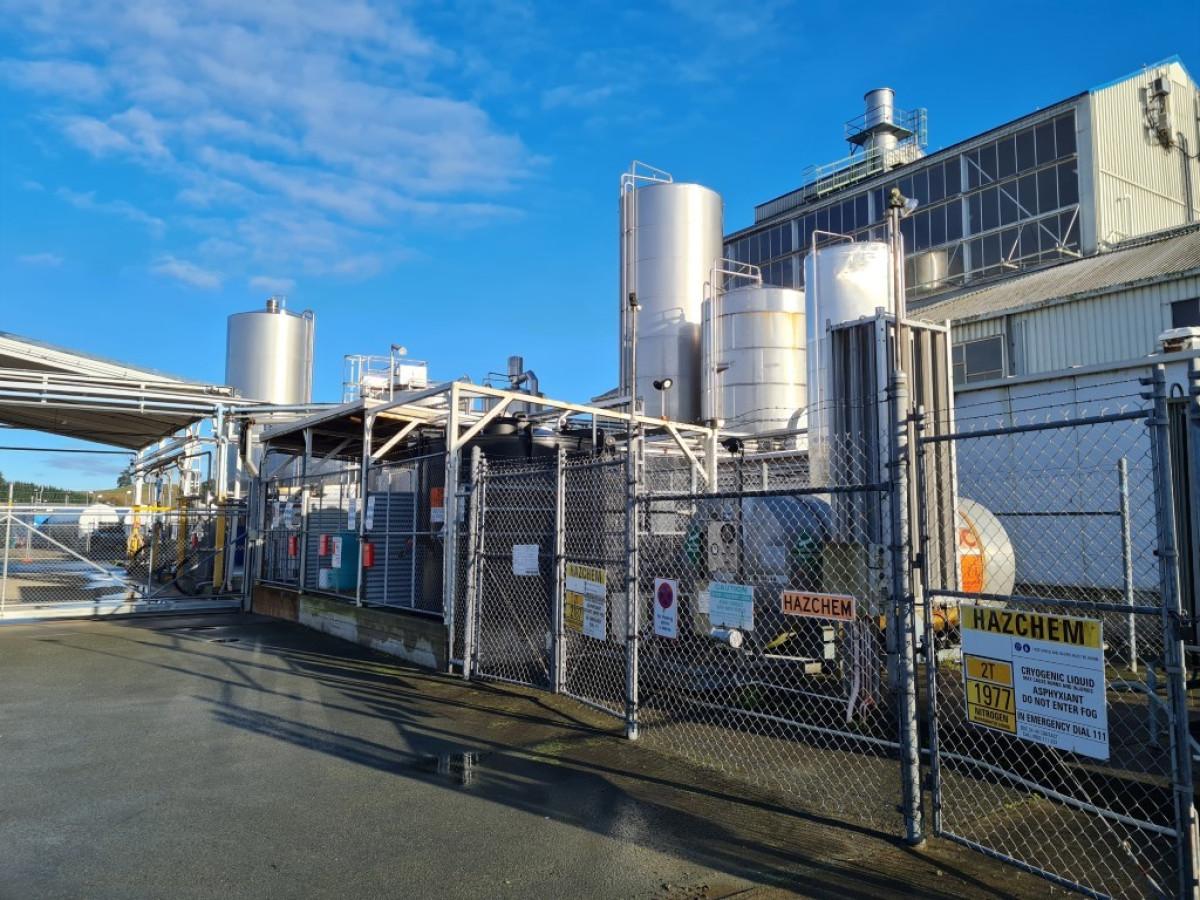
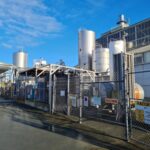
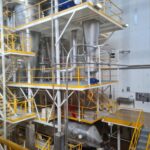
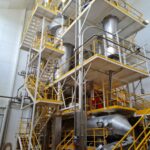
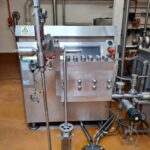
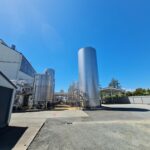
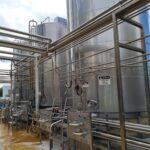
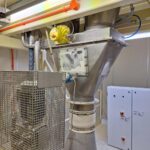
This milk powder plant was originally designed to produce Skimmed Milk Powder in 1976.
More recently, it was capable of handling 13,000 litres of intake milk per hour, and was producing either Whole Milk Powder, Skimmed Milk Powder and also Butter Milk Powder.
The separation/standardisation system was capable of handling 22,000 litres per hour, utilising an Alfa MRX 318 Separator in conjunction with a BASK Standardisation System.
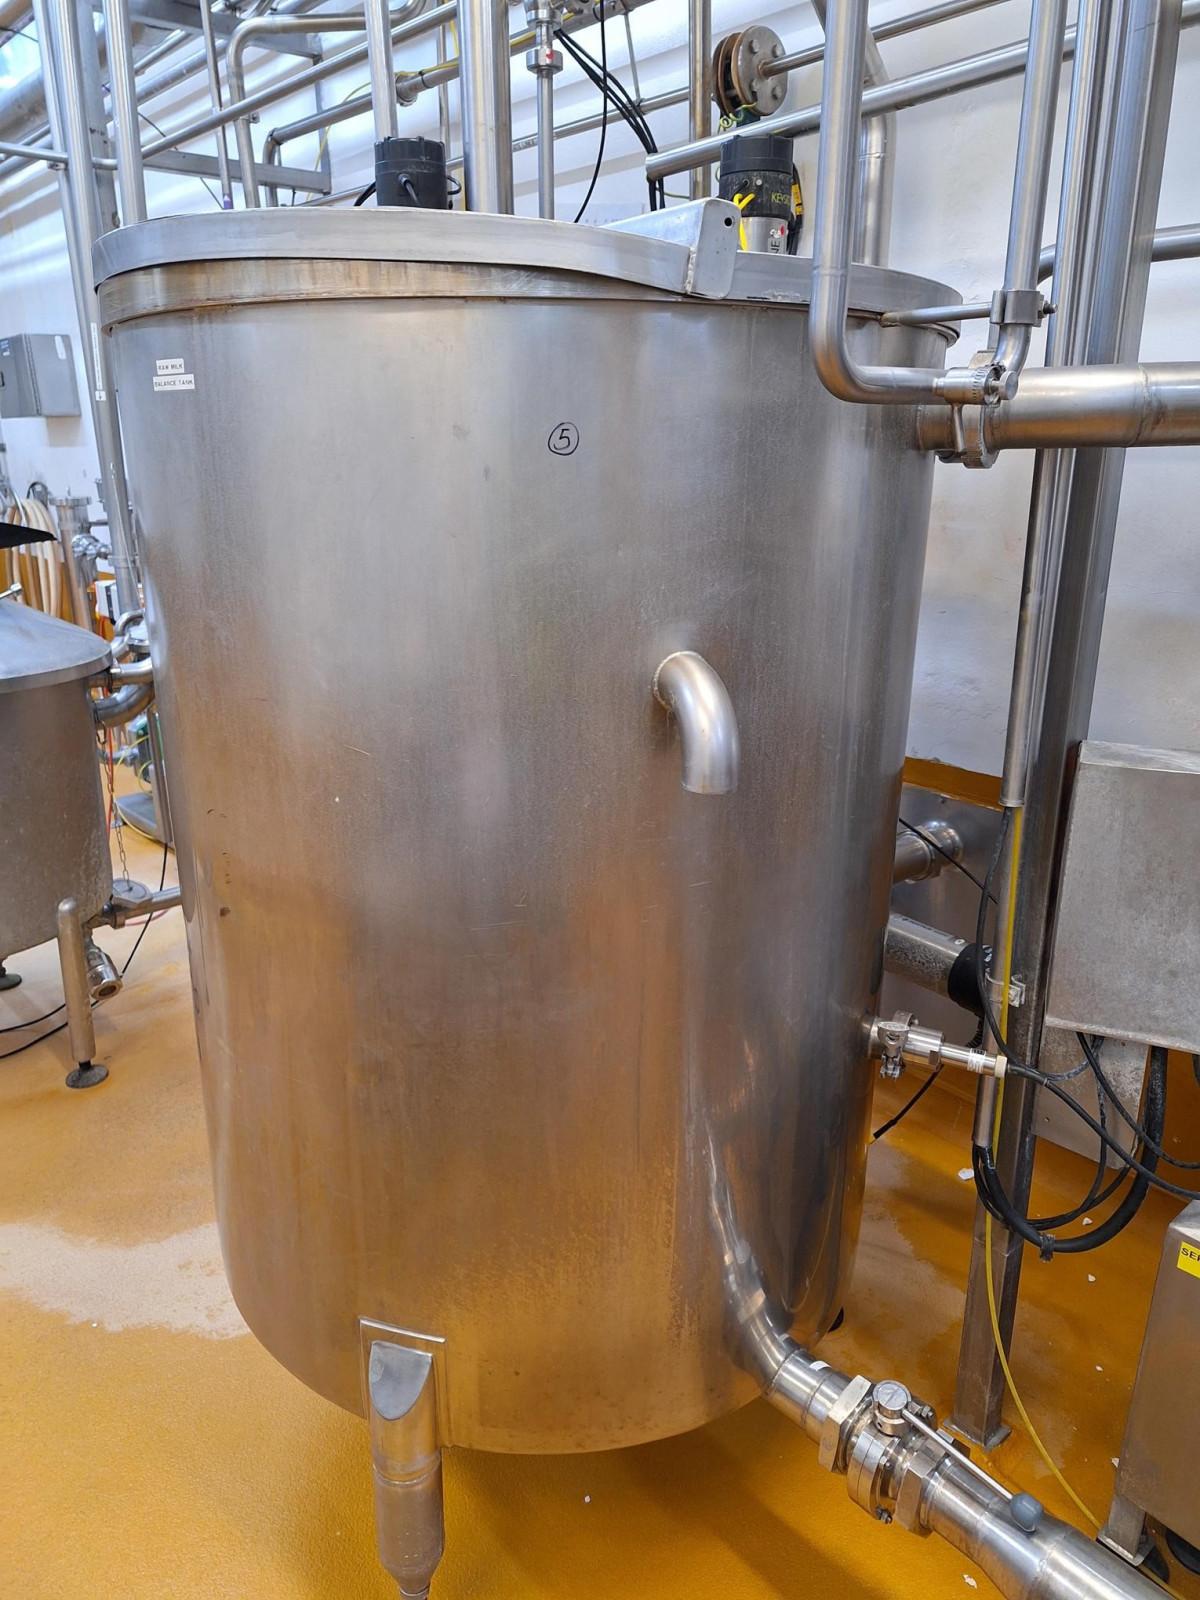
The Pasteuriser Tank (Internal Coils) preheats the product to 60 Deg C, before passing on to the Evaporator.
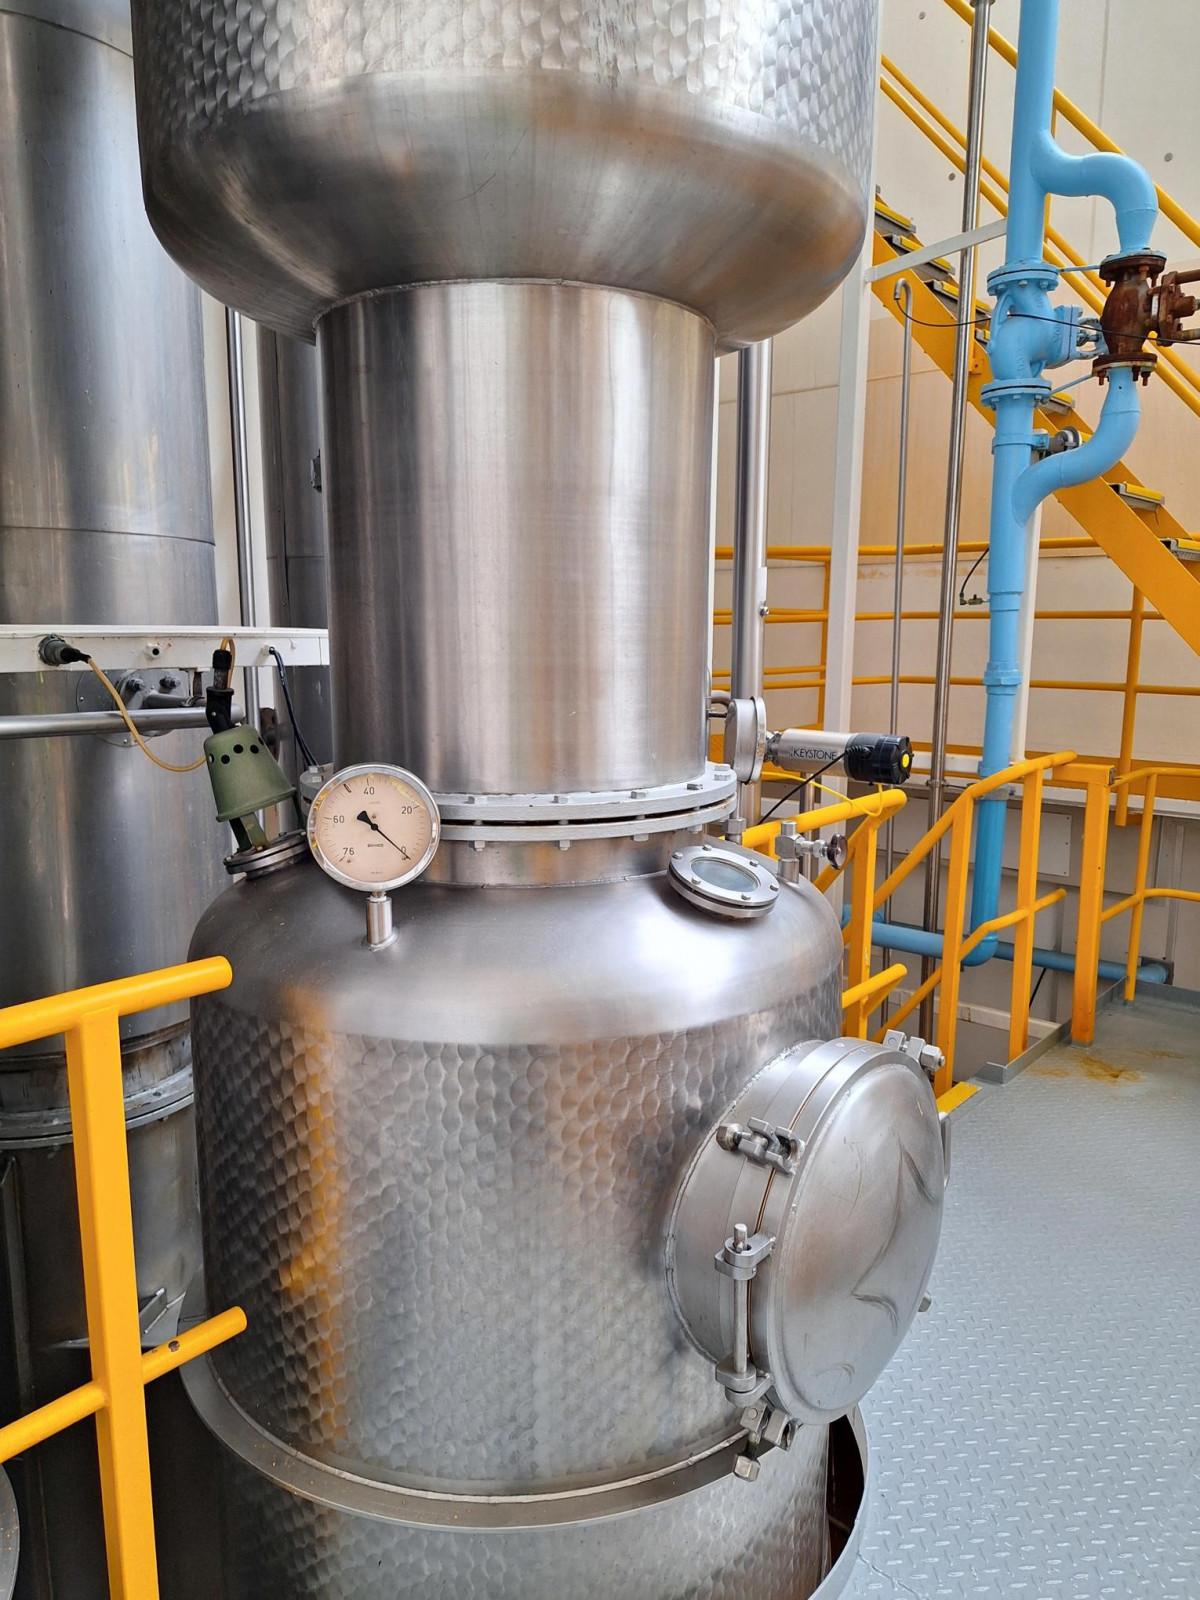
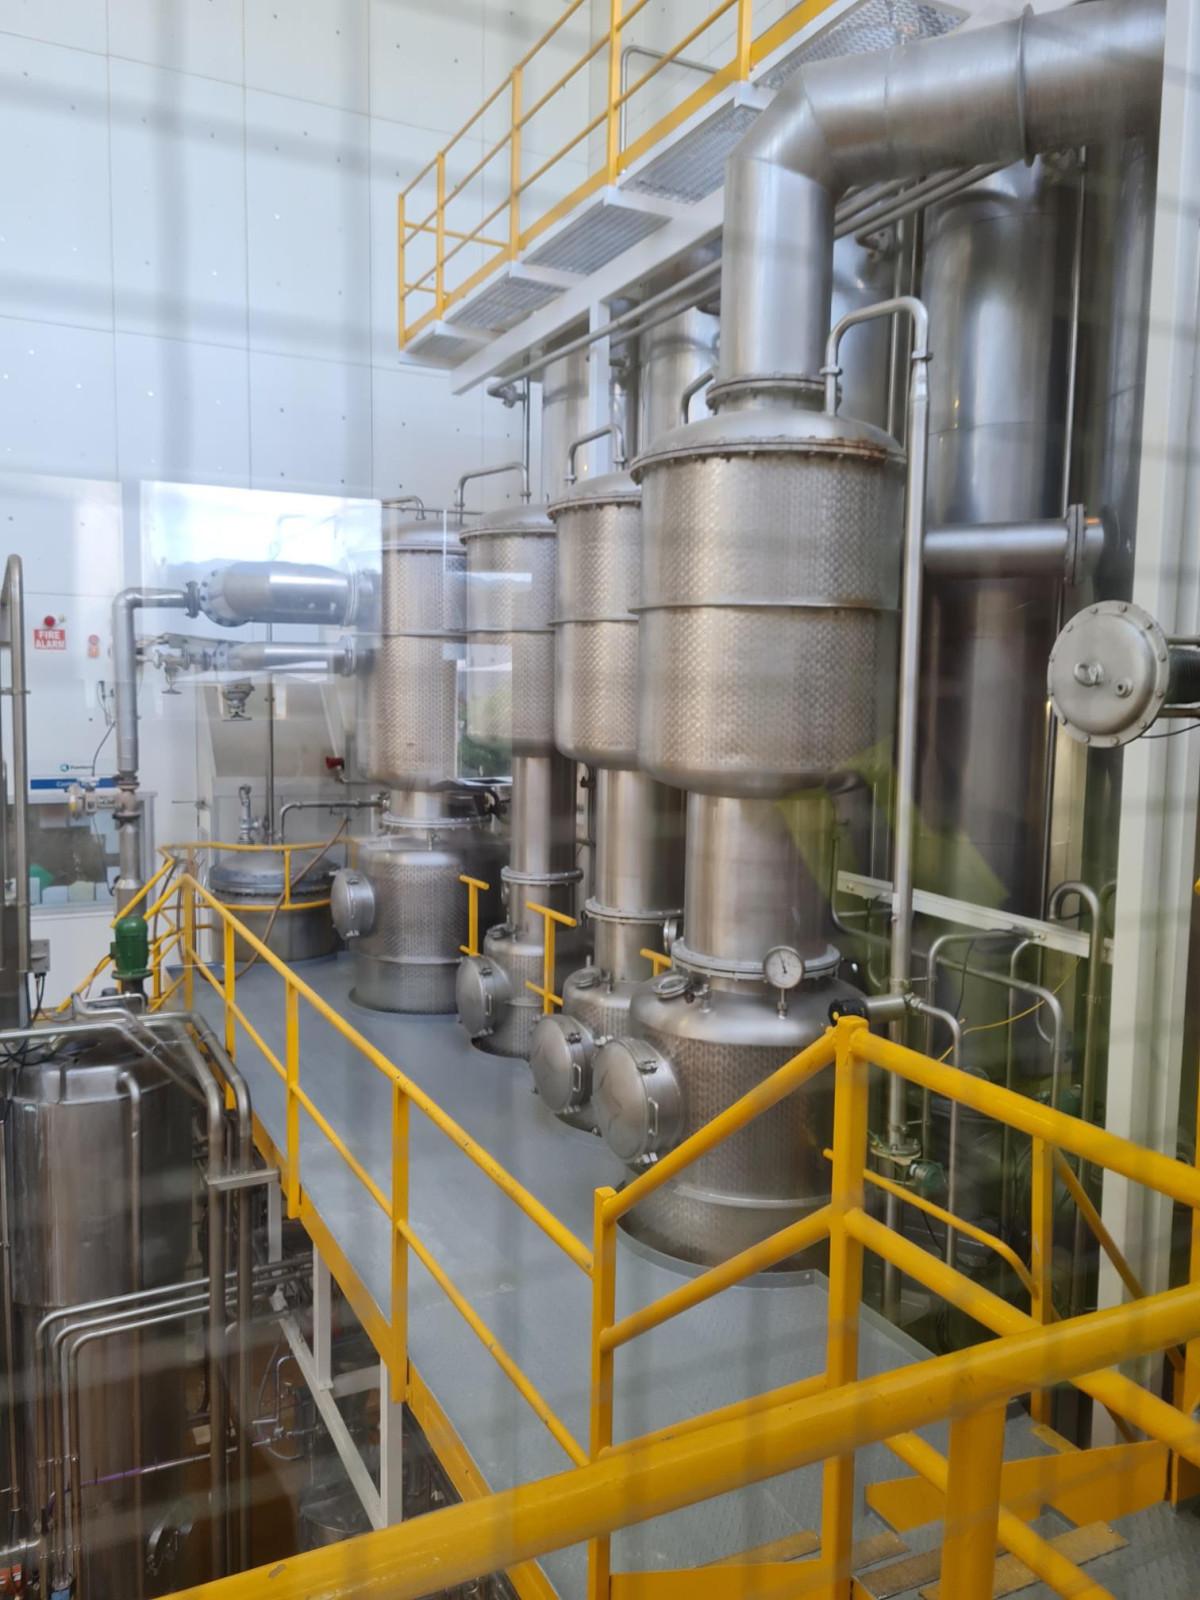
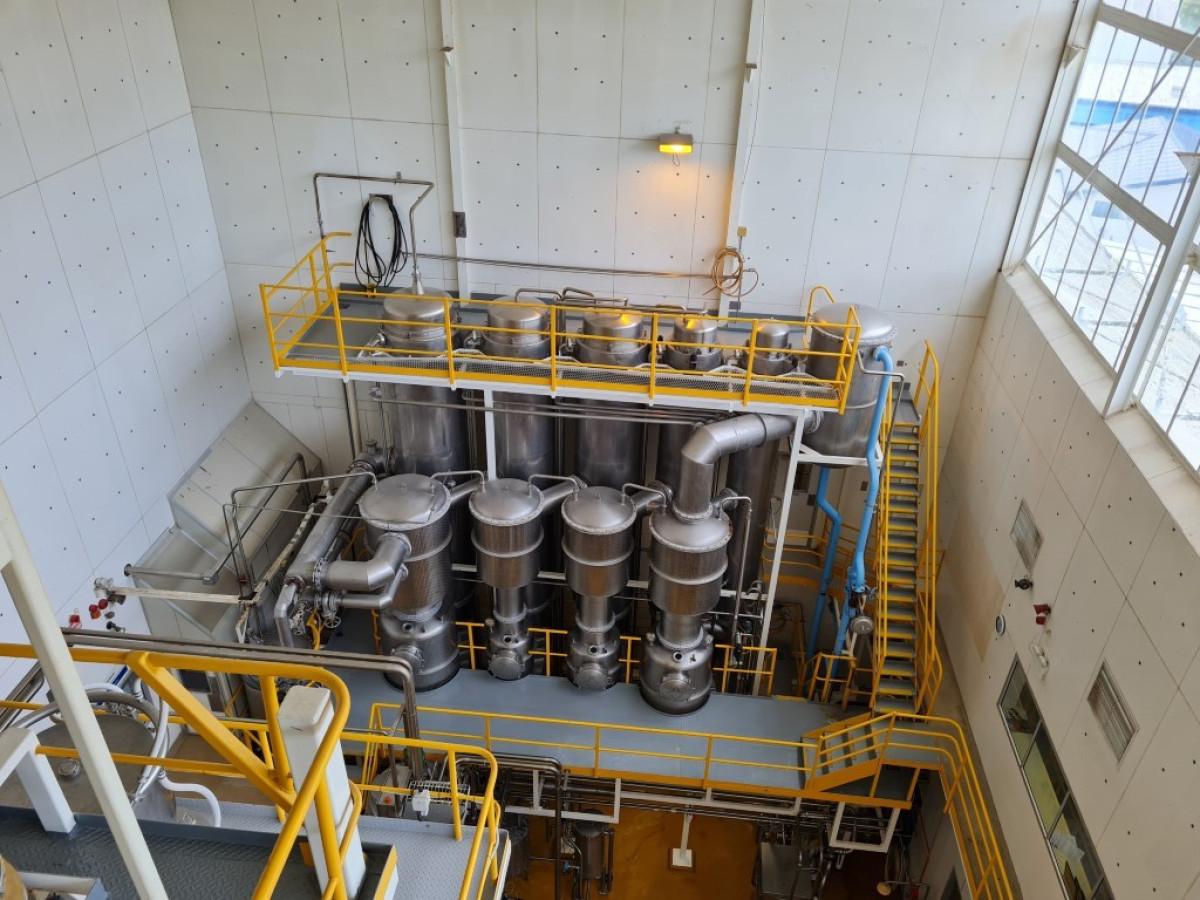
The Evaporator is a 4 Affect Van de Ploegh, rated at 1.5 tons per hour. One Affect was configured with 2 Passes for Whole Milk Powder, divided on a Distribution Plate.
New Fristram Pumps were installed in 2020.
A Breakout Tank was installed in 2014, after the Evaporator, with the aim of removing some of the steam prior to passing to the Drier.
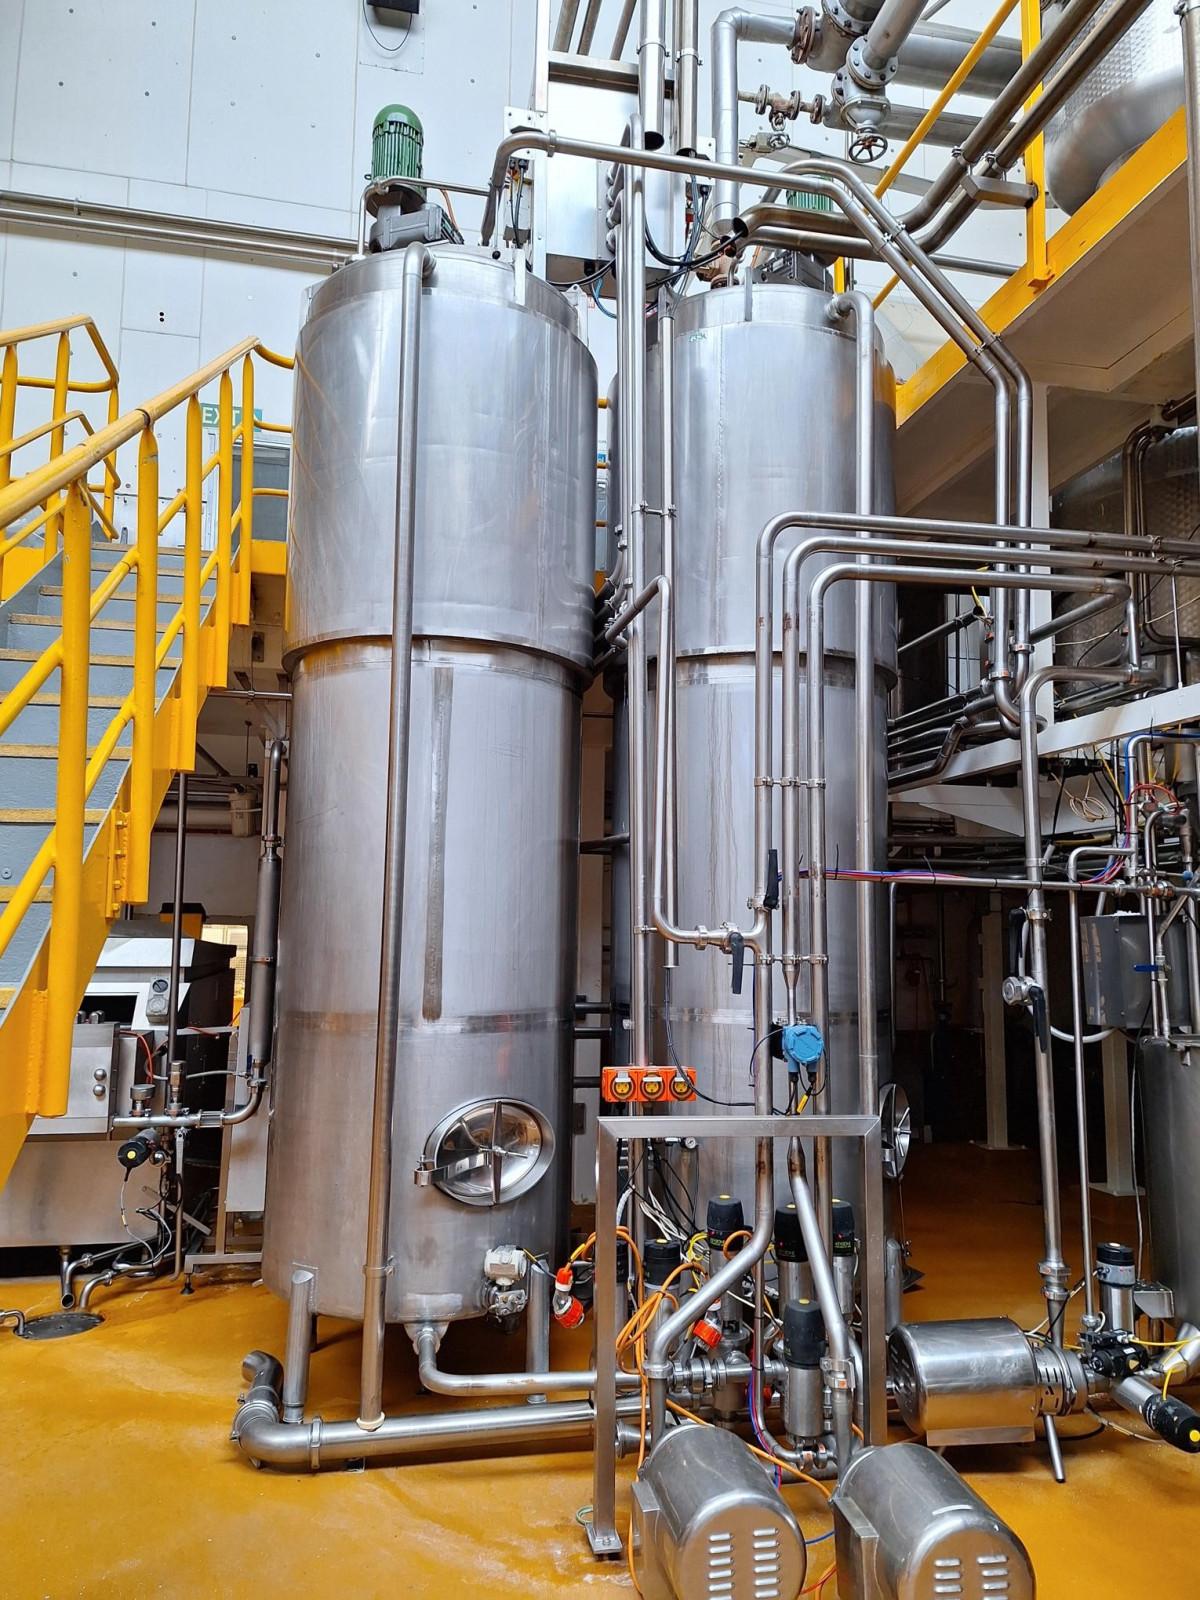
Two 3,000 litre Concentration Mixing Tanks, with Full Length Agitators, are used to feed the Drier while the Evaporator is being cleaned. The Agitators were installed in 2007.
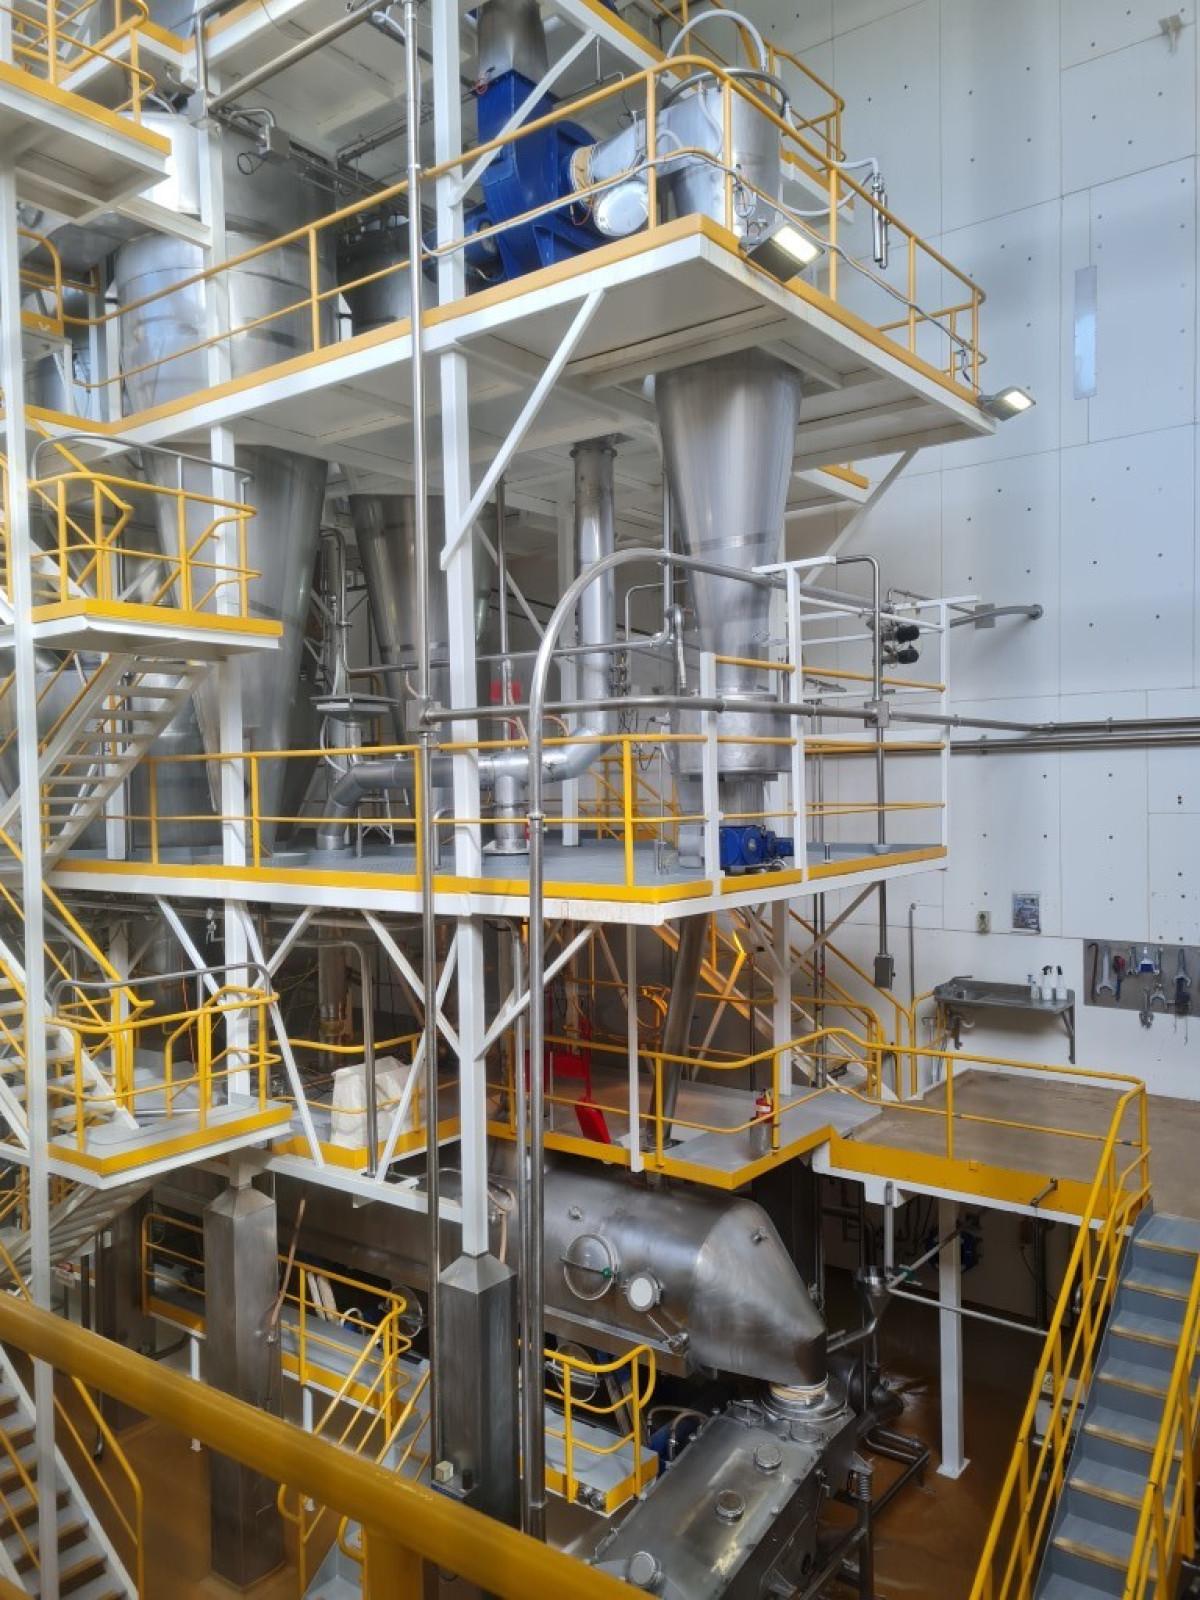
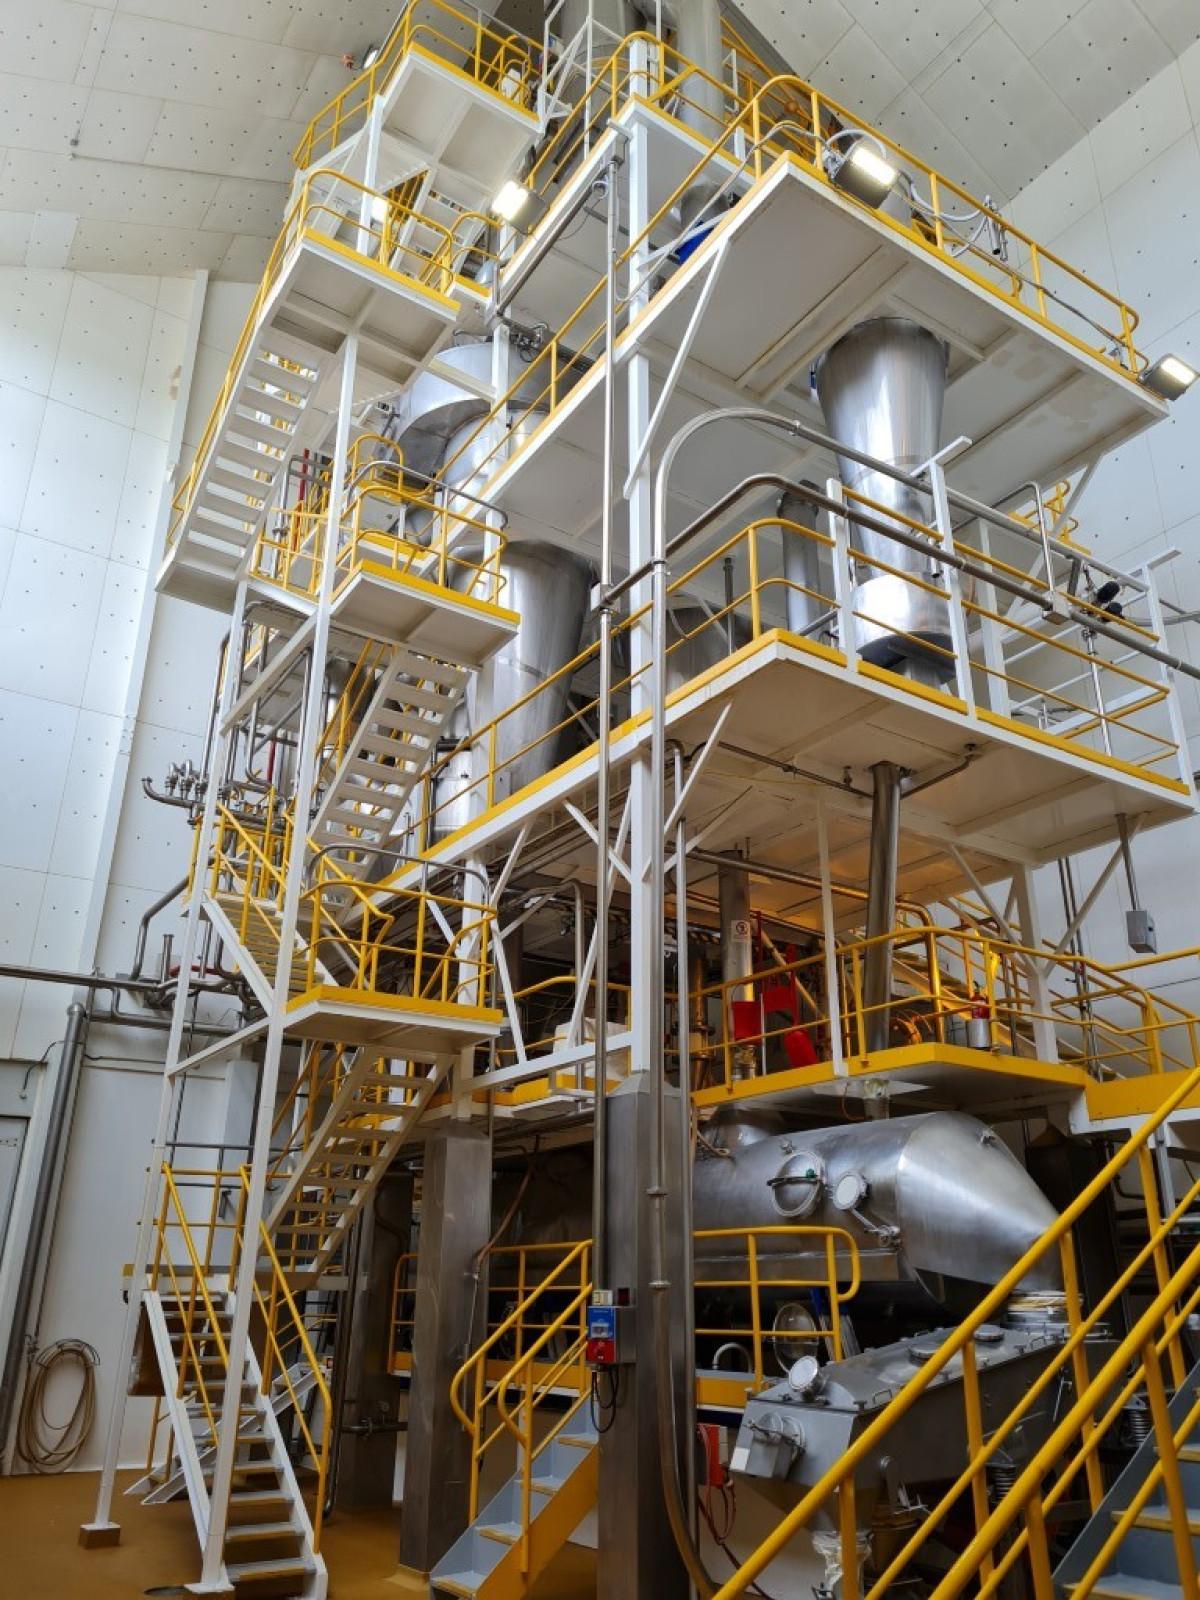
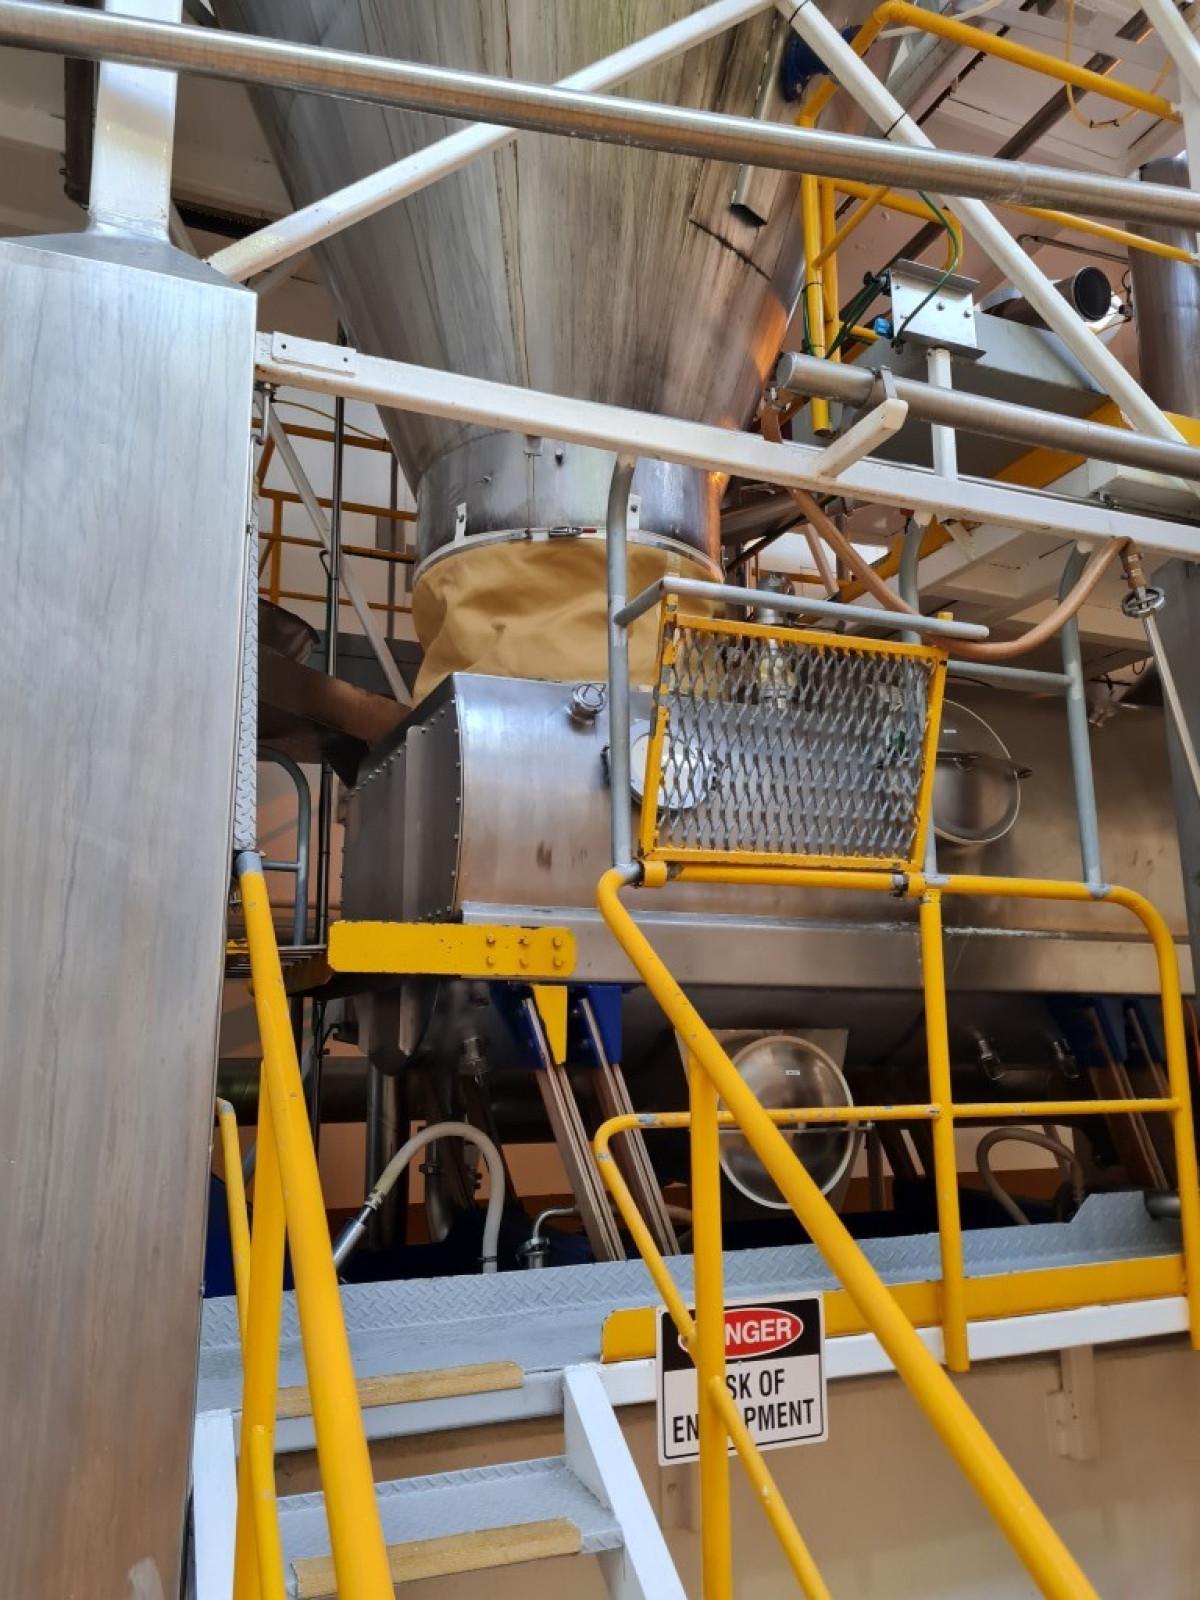
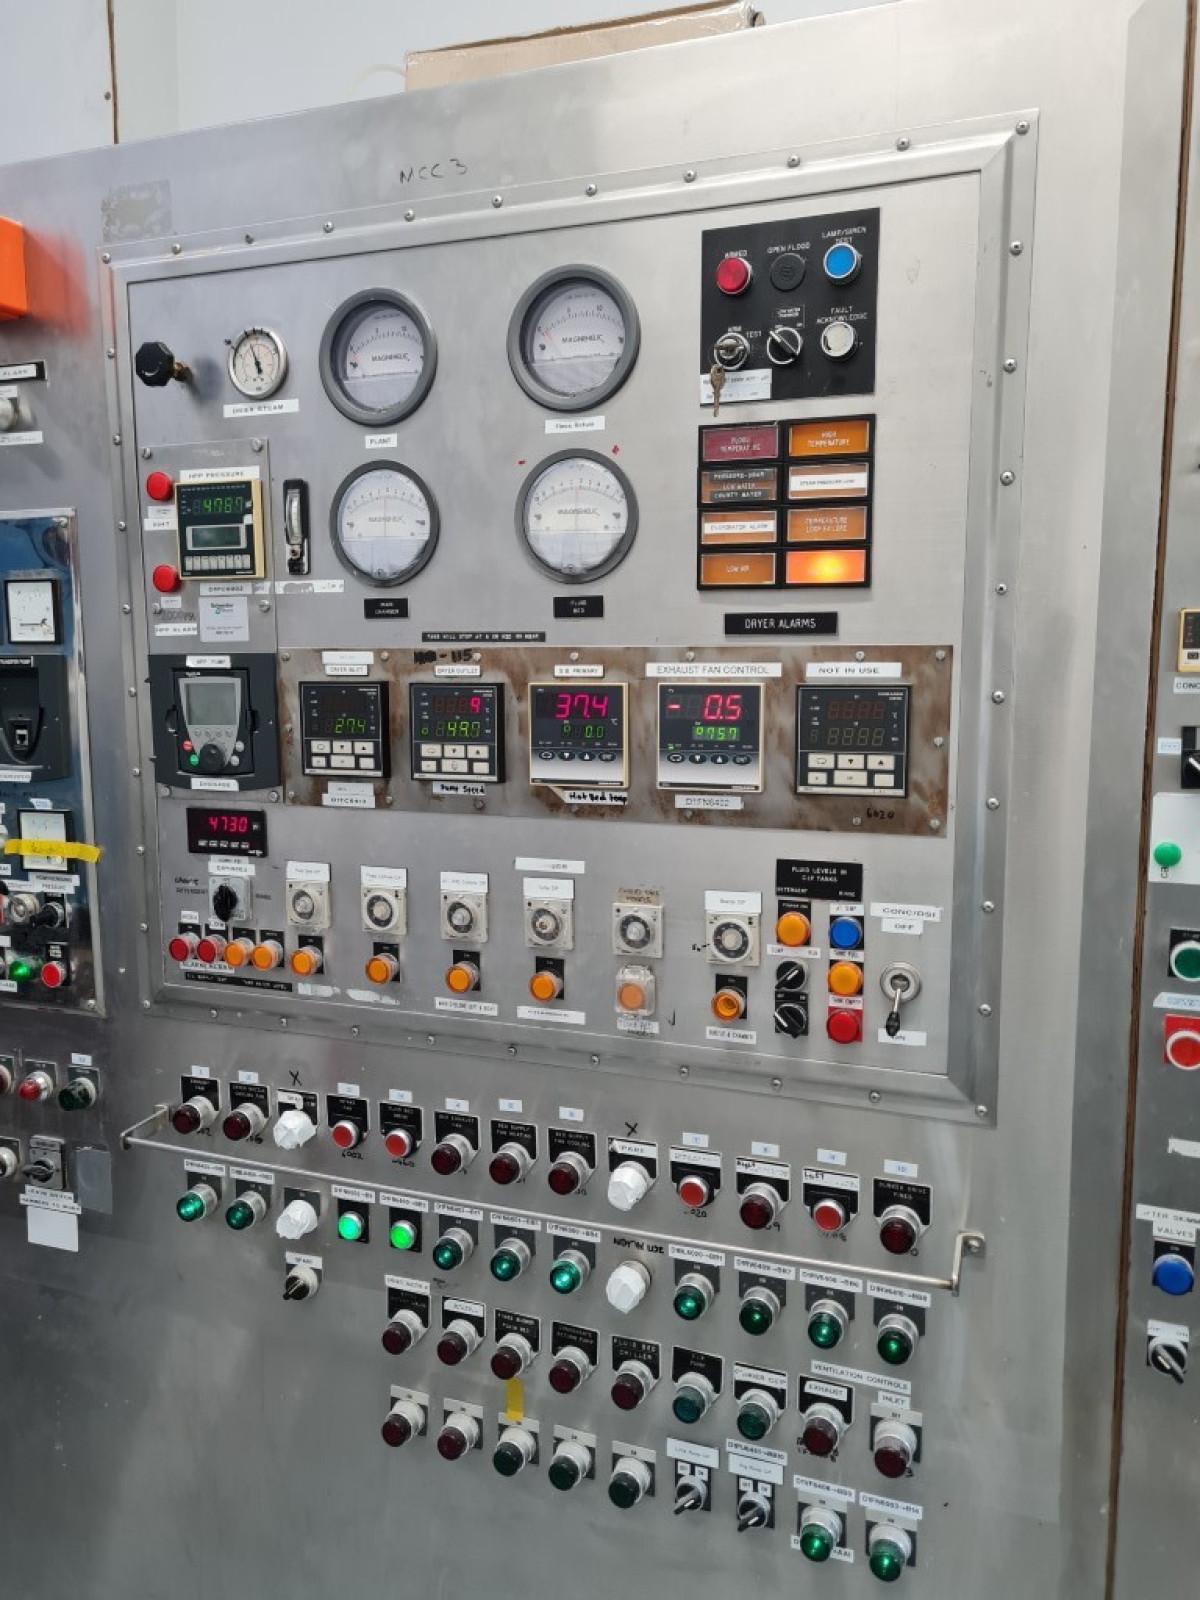
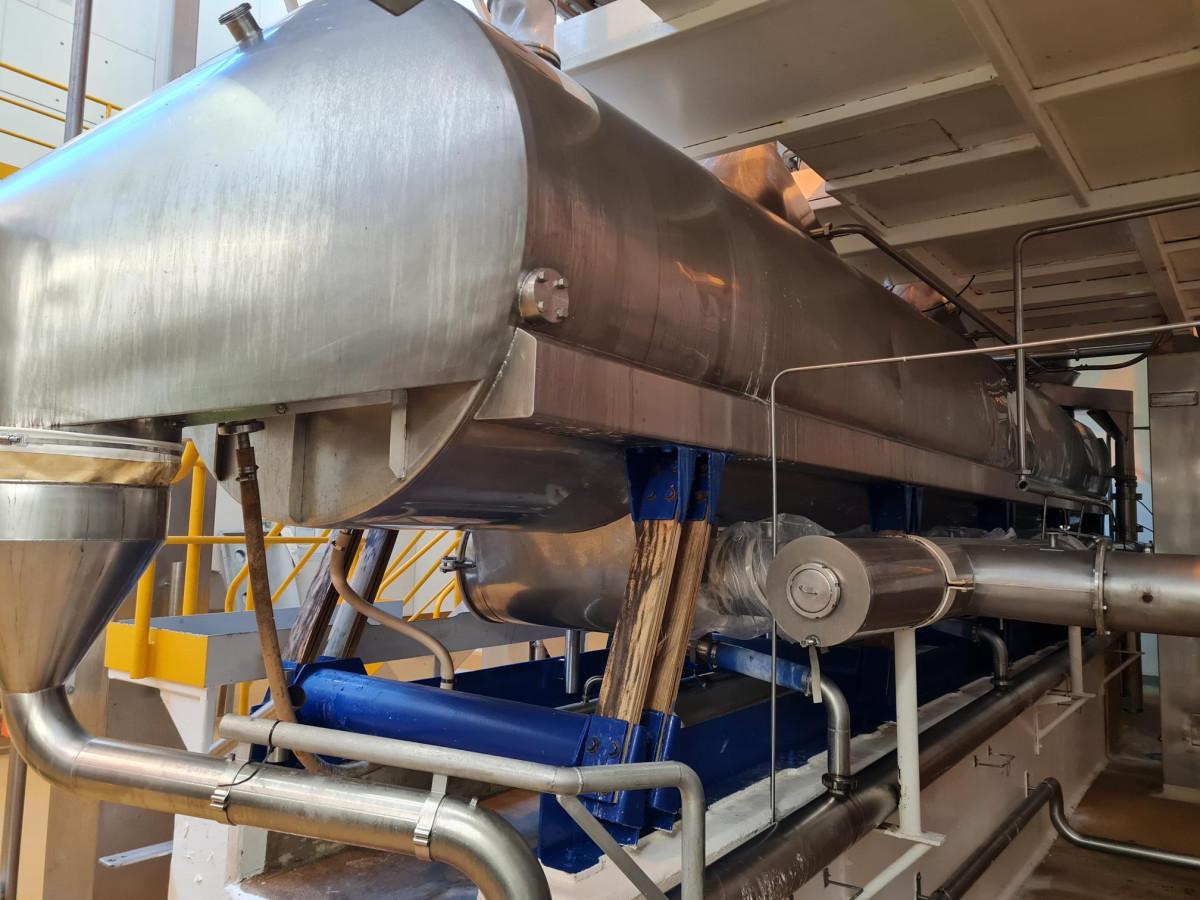
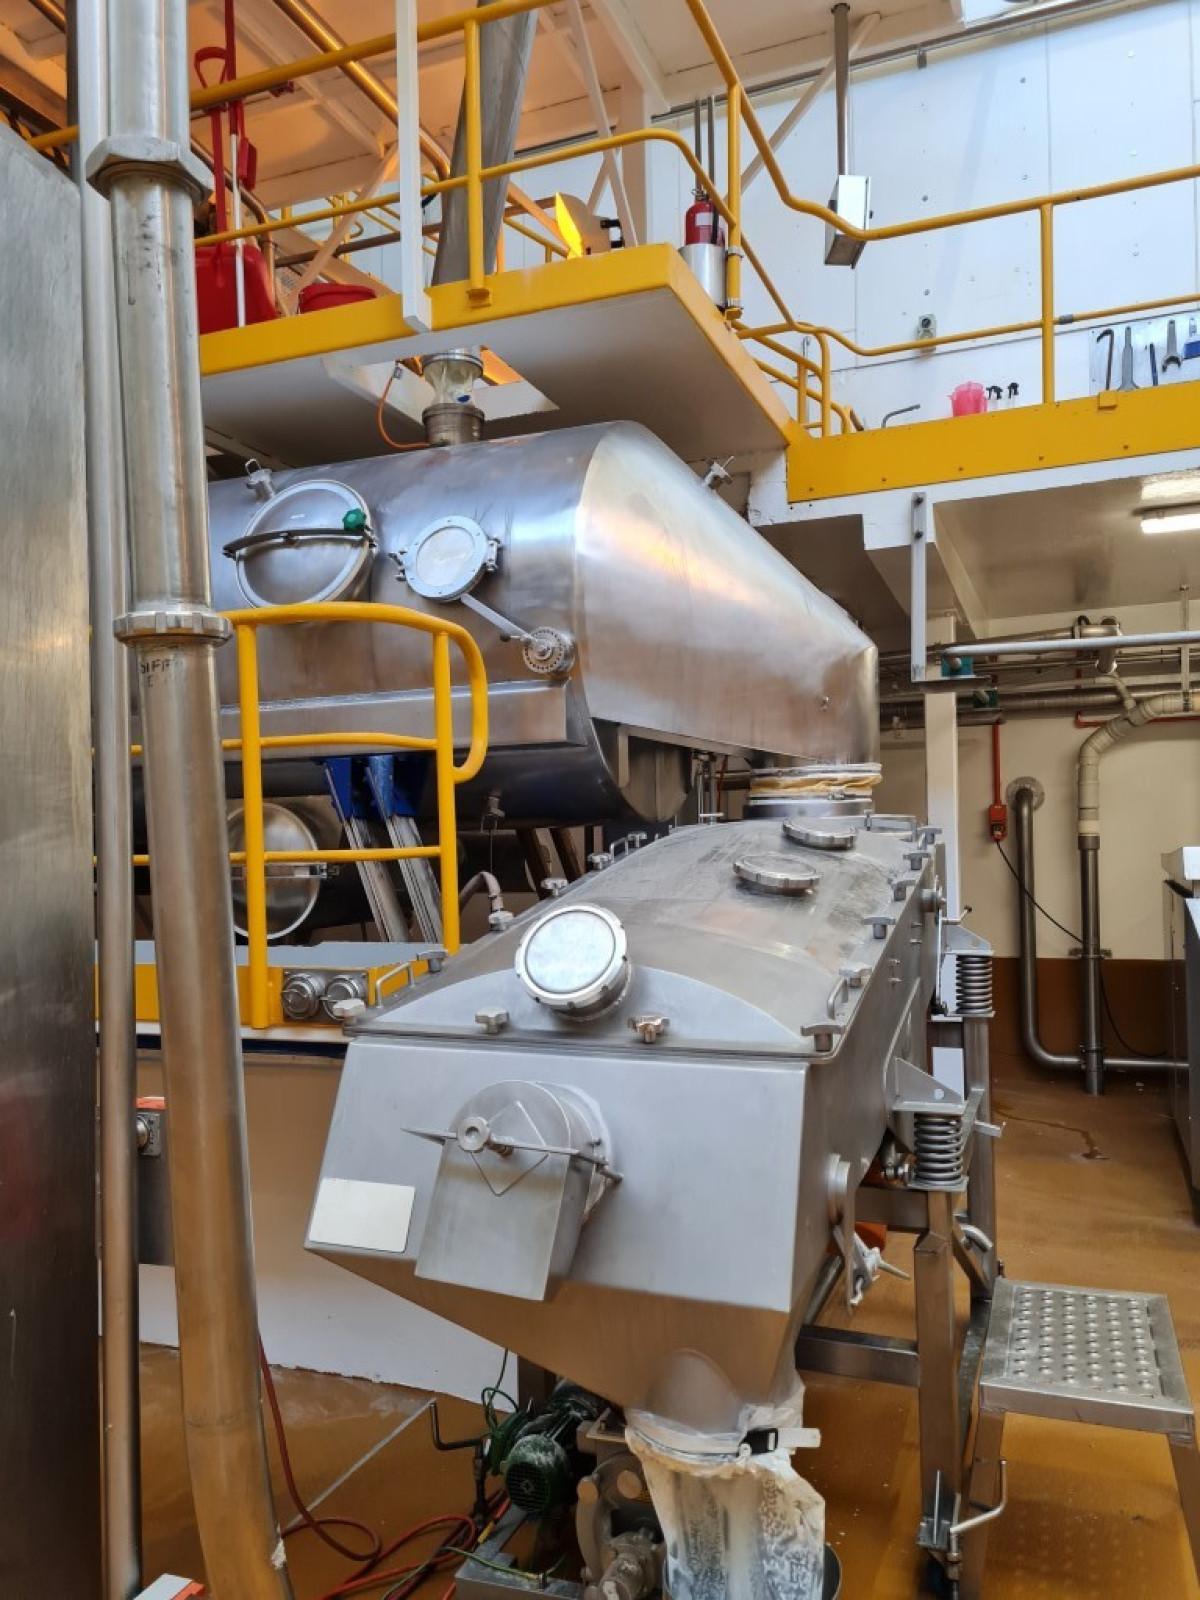
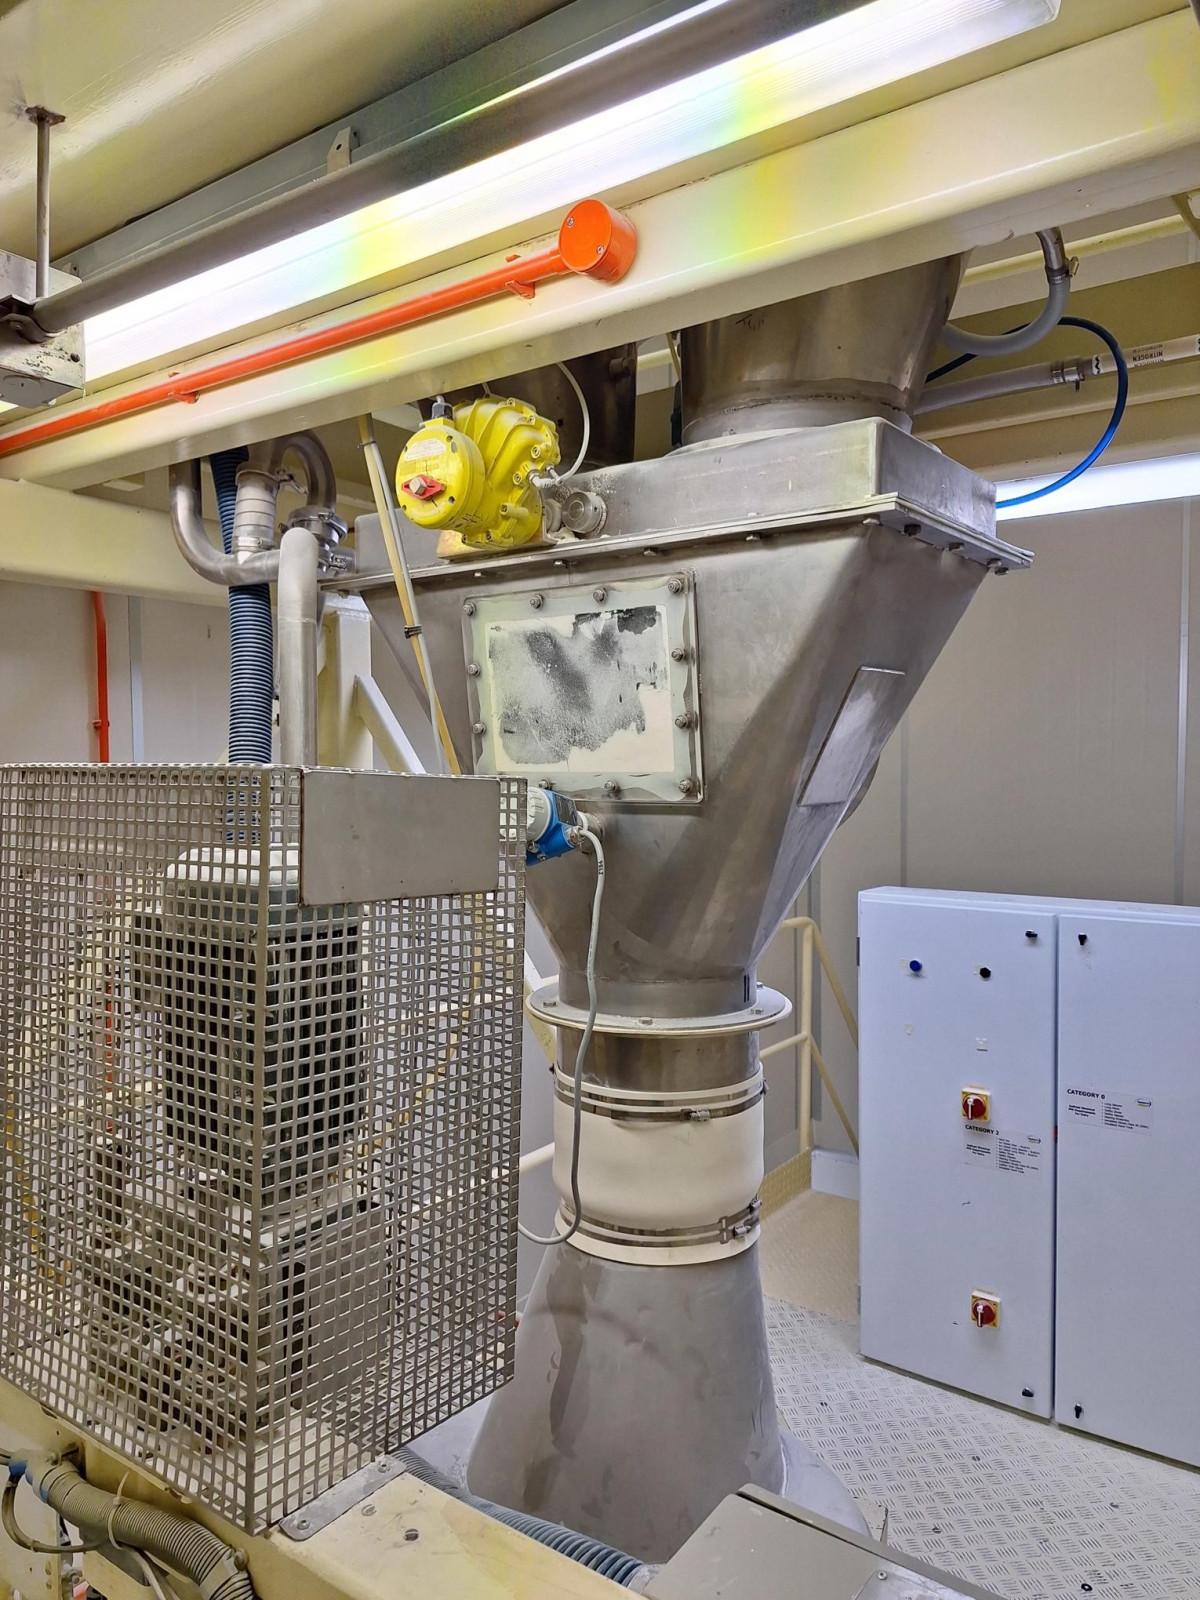
The Drier is a De Laval unit rated at 1 ton per hour. Tall Form Single Nozzle. Infeed 2370 litres per hour at 51% Solids, with a target of 52 – 54%. DSI (Direct Steam Injection), Inlet Temperature of 90 Deg C. No Bag House, 2 x Cyclones off of the drier as Transition Silos.
VAV Sifter (installed 1990s) rated at 3 tons per hour, accepts powder from the Fluid Bed, and has a Rotary Valve to transfer any Fines back into the Fluid Bed.
The main flow of powder is transferred via a further Rotary Valve to the Powder Silos (Unavailable) with a total of 3 Dust Collectors, and 3 DMN Plug-type line Diverter Valves, included.